

Ophthalmic Suspension Manufacturing
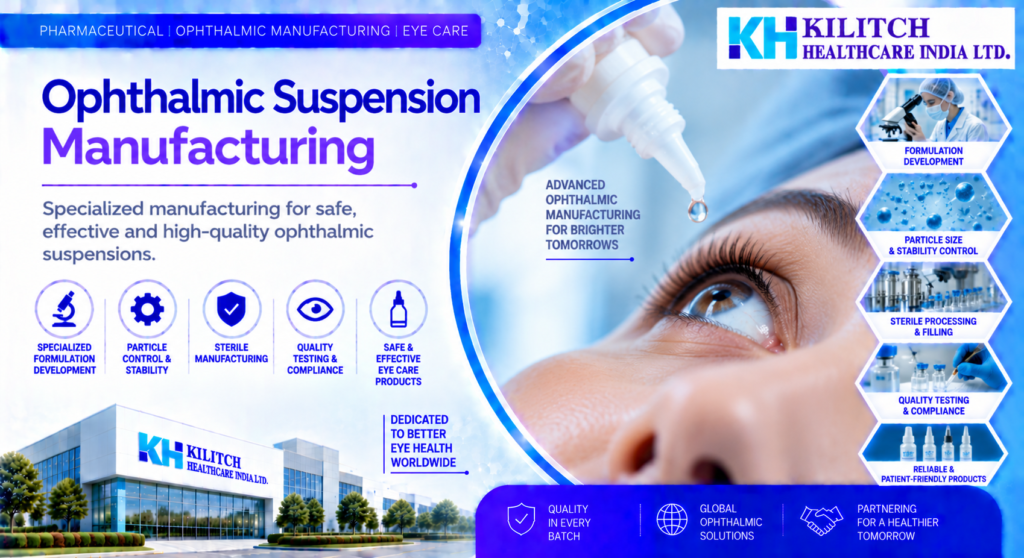
Introduction: Why Ophthalmic Suspensions Require Specialized Manufacturing Ophthalmic suspension manufacturing involves the controlled production of sterile eye products in which finely divided drug particles are dispersed within a suitable liquid vehicle. Unlike a simple ophthalmic solution, a suspension contains insoluble or sparingly soluble particles, making particle characteristics, uniformity, sterility, resuspendability and dose delivery important considerations. Kilitch Healthcare works across specialized ophthalmic formulations, making an integrated approach to formulation, sterile processing, filling and quality control particularly relevant for these products. What Is an Ophthalmic Suspension? An ophthalmic suspension is a sterile liquid dosage form containing drug particles that are dispersed rather than completely dissolved. The formulation is designed so the particles remain suitably distributed during handling and can be resuspended when required. Its performance depends on the properties of the active ingredient, excipients, particle size, vehicle and container system. Because the product is intended for ocular administration, development must consider both pharmaceutical performance and patient safety. The formulation needs to maintain appropriate physical characteristics during storage while supporting consistent administration. This makes ophthalmic suspension development a combination of formulation science, sterile manufacturing and product-specific quality control. Key Considerations in Ophthalmic Suspension Manufacturing Particle Size and Distribution Particle characteristics can influence the physical stability and performance of an ophthalmic suspension. Particle size distribution, morphology and surface properties may affect sedimentation, redispersibility and the consistency of the administered dose. Development teams therefore need to establish suitable particle characteristics for the specific drug product. Suspension Stability A suspension naturally tends to settle over time, so the formulation must be designed to support appropriate physical stability and easy redispersion. Vehicle properties, suspending agents and other excipients can influence how particles behave during storage. Stability studies help establish whether the formulation continues to meet its defined requirements throughout its intended shelf life. Sterility and Microbial Control Sterility is fundamental for ophthalmic products. Manufacturing controls must address the risk of microbial contamination across formulation preparation, processing, filling, container closure and finished-product handling. Facility controls, validated procedures, environmental monitoring and appropriate testing work together to support the required sterility assurance. Ophthalmic Suspension Manufacturing Process 1. Raw-Material and Active-Ingredient Preparation The manufacturing process begins with controlled handling of the active pharmaceutical ingredient and excipients. Material identity, quality and suitability are established against approved specifications. For a suspension, the physical characteristics of the active ingredient can be particularly important because they directly influence dispersion and product performance. 2. Particle Processing and Dispersion The active ingredient may require appropriate particle processing before it is incorporated into the formulation. The objective is to achieve the desired particle characteristics and distribute the drug uniformly throughout the vehicle. Mixing parameters, order of addition and processing conditions need to be established according to the product. 3. Formulation Preparation The formulation is prepared using controlled procedures for the vehicle, excipients and active ingredient. Parameters such as mixing time, temperature, concentration and processing sequence may affect suspension quality. Consistent process control helps reduce variability between batches and supports reproducible product characteristics. 4. Sterile Processing and Filling Once the formulation is ready, the product is processed and filled under suitable controlled conditions. Depending on the formulation and manufacturing strategy, filtration or other product-specific controls may be used where appropriate. Filling accuracy, container handling and equipment performance are important for maintaining consistent product quality. 5. Stoppering, Inspection, and Packaging After filling, containers are closed using the specified closure system and inspected according to established requirements. Packaging protects the product during storage, transportation and handling. The container and closure must also remain compatible with the formulation and support product integrity throughout its intended shelf life. Quality Control in Ophthalmic Suspension Manufacturing Assay and Content Uniformity Analytical testing helps confirm that the drug product contains the intended amount of active ingredient and meets established specifications. For a suspension, sampling and testing approaches should account for the dispersed nature of the formulation so that product uniformity can be evaluated appropriately. Particle and Physical Characteristics Physical testing can evaluate characteristics relevant to suspension performance, including particle size, appearance, redispersibility and other product-specific attributes. These assessments help determine whether the formulation remains within its defined quality profile during development and stability testing. Sterility and Safety Testing Ophthalmic products require appropriate microbiological and quality controls. Testing and environmental monitoring are used alongside controlled manufacturing practices to verify that the product and process meet established requirements. The exact testing programme depends on the product and applicable specifications. Formulation Development Challenges Developing an ophthalmic suspension can involve balancing several formulation requirements at once. The product must maintain suitable particle characteristics, remain adequately dispersed, support acceptable administration and retain stability during storage. Changes to one component can influence other properties, so formulation optimization requires a systematic development approach. Container and delivery considerations are also important. The selected bottle, dropper or other delivery configuration should work with the suspension and help provide consistent administration. Compatibility studies can help identify potential interactions between the formulation and packaging materials before commercial production. Why Integrated Ophthalmic Manufacturing Matters Ophthalmic suspension manufacturing requires close coordination between formulation development, sterile processing, filling, analytical testing and packaging. An integrated pharmaceutical manufacturing approach can help connect these activities and reduce the risk of development decisions creating challenges during commercial production. This becomes especially important when a formulation moves from laboratory or pilot work into routine manufacturing. Equipment characteristics, batch size, process controls and material handling can change with scale. Early consideration of manufacturing requirements can therefore support a more controlled transition to commercial supply. Choosing an Ophthalmic Manufacturing Partner Companies evaluating an ophthalmic manufacturing partner should consider more than basic production capacity. Relevant factors include experience with sterile ophthalmic formulations, formulation-development support, particle and suspension expertise, filling capabilities, analytical testing, quality systems and packaging knowledge. A partner with experience across these areas can help align product development with manufacturing requirements. For businesses exploring ophthalmic pharmaceutical manufacturing, reviewing the manufacturer’s formulation and production capabilities can help determine whether its infrastructure is appropriate for the intended product. Ophthalmic Suspension Manufacturing at Kilitch Healthcare Kilitch Healthcare works across
Nasal Drug Delivery System
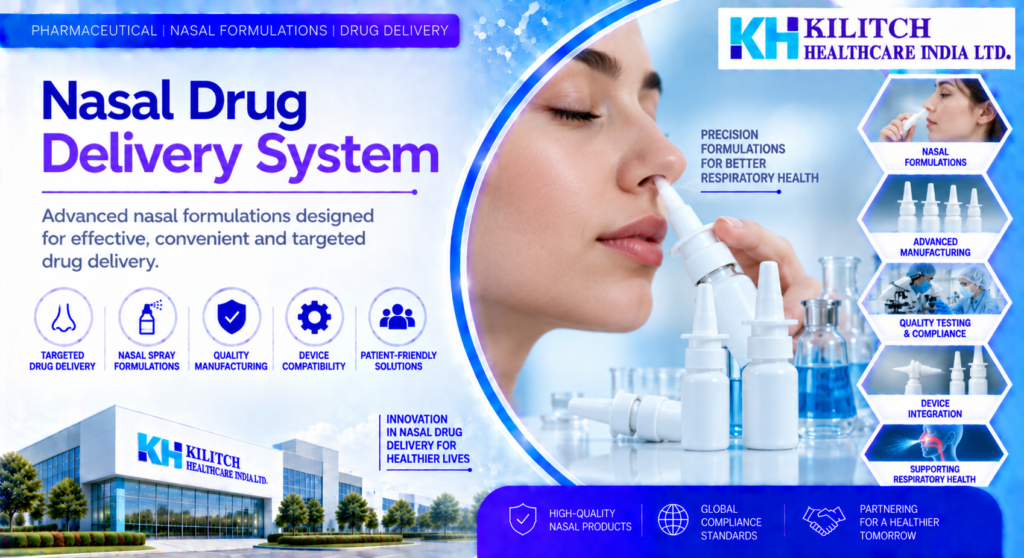
Introduction: Why Nasal Drug Delivery Matters A nasal drug delivery system is designed to administer a pharmaceutical formulation through the nasal route, using the nasal cavity as the intended site of delivery. Depending on the product, this route can support local treatment or systemic drug delivery. Developing a reliable nasal product requires more than selecting a spray device; formulation properties, dose delivery, packaging, manufacturing controls and product quality all need to work together. Kilitch Healthcare operates across specialized pharmaceutical categories, including nasal formulations, alongside sterile injectables, ophthalmic products and prefilled syringes. What Is a Nasal Drug Delivery System? A nasal drug delivery system combines a pharmaceutical formulation with an appropriate method of administering that formulation through the nose. The system may include the drug product, container, closure and delivery device, depending on the dosage form. A nasal spray is one common format, but the broader concept is the complete product and delivery arrangement rather than the device alone. For a pharmaceutical company, this means formulation development and delivery-system selection should be considered together. Factors such as the active ingredient, concentration, solubility, viscosity, dose requirements, intended use and packaging can influence the final product design. Advantages of Nasal Drug Delivery Rapid and Convenient Administration Nasal administration can provide a convenient alternative to other routes when the formulation and therapeutic application are appropriate. A product can be administered directly through the nasal route without requiring the patient to swallow a tablet or use an injection. Potential for Local or Systemic Delivery The nasal route can be used for products intended to act locally in the nasal passages, while selected formulations may be developed for systemic exposure. The appropriate approach depends on the drug substance, formulation characteristics and intended therapeutic objective. These requirements should be established early so the product is designed around its intended performance. Patient-Friendly Delivery A well-designed nasal product can offer a practical administration experience when the formulation, dose and delivery device are appropriately matched. Ease of use, consistency of delivered dose and packaging design can all influence how effectively the final product supports routine administration. Key Components of a Nasal Drug Delivery System Formulation The formulation is central to product performance. Solubility, pH, viscosity, concentration and other characteristics can influence processing and delivery. Excipients must be selected appropriately for the intended product, while stability considerations should be evaluated under the proposed storage conditions. Container and Closure The container and closure system protects the formulation during storage and handling. Compatibility between the formulation and packaging materials should be evaluated because interactions can affect product quality over time. Delivery Device The delivery device is an important part of a nasal product because it determines how the formulation is administered. Device characteristics can influence dose consistency, spray performance and user experience. For this reason, device selection should be assessed alongside formulation development rather than being treated as a final packaging decision. Nasal Formulation Development Considerations Formulation Properties A nasal formulation needs to maintain suitable physical and chemical characteristics throughout development and storage. Development teams may evaluate parameters such as pH, viscosity, drug content, appearance, solubility and stability according to the product. Device Compatibility Formulation and device compatibility can affect the performance of the finished product. The formulation must work appropriately with the selected components, while the device must provide the intended delivery characteristics. Evaluating both elements together can help identify potential manufacturing or performance issues before commercial production. Manufacturing Process for Nasal Pharmaceutical Products Nasal pharmaceutical manufacturing generally involves controlled preparation of the formulation, appropriate processing, filling into the selected container or delivery system, packaging, inspection and quality testing. Depending on the product, operations can include controlled mixing, dissolution, filtration or other product-specific steps. Pharmaceutical manufacturing capabilities need to be aligned with the formulation, filling requirements and intended market. 1. Raw-Material and Component Control Active ingredients, excipients, containers, closures and delivery components all contribute to the final product. Their identity, quality and suitability should be controlled according to established specifications. Component compatibility is particularly important where the formulation comes into direct contact with packaging or device materials. 2. Controlled Formulation Preparation The formulation is prepared using defined procedures and process parameters. Mixing, dissolution, temperature, filtration and other operations may be relevant depending on the formulation. Consistent process control helps reduce batch-to-batch variation and supports reproducible product quality. 3. Filling and Assembly The prepared formulation is transferred into the selected container or delivery system under controlled conditions. Fill quantity, equipment performance, component handling and line controls can influence the consistency of the finished product. Assembly procedures should also ensure that the delivery system functions as intended. 4. Packaging and Inspection Packaging protects the product during storage, transport and handling. Finished units are inspected for relevant physical and packaging attributes, while manufacturing records are reviewed as part of the quality process. Appropriate controls help establish that the product meets its defined specifications before release. Quality Considerations for Nasal Drug Delivery Systems Dose and Delivery Consistency A nasal product should deliver the intended quantity consistently according to its established specifications. The interaction between formulation, container and delivery device can influence this performance. Testing and process controls should therefore reflect the characteristics that are critical to the finished product. Stability and Packaging Compatibility Stability studies help establish how the product behaves during its proposed storage period. The programme may consider drug content, degradation, formulation characteristics and compatibility with the container or delivery system. Packaging should provide suitable protection against relevant environmental factors and maintain product quality. Documentation and Process Control Controlled documentation supports traceability throughout development and manufacturing. Specifications, batch records, test results, procedures and quality records provide evidence that the product has been produced and evaluated according to established requirements. Why Integrated Development and Manufacturing Matters Nasal products bring together formulation science, delivery-device considerations and manufacturing requirements. When these areas are developed separately, practical issues can emerge later in the project. An integrated approach allows formulation, packaging, filling, quality and commercial manufacturing considerations to be reviewed together. For companies evaluating a partner, an integrated
Lyophilized Drug Manufacturing: Process
Introduction: What Is Lyophilized Drug Manufacturing? Lyophilized drug manufacturing is a specialized pharmaceutical process used to convert a prepared drug formulation into a dry, stable product through controlled freeze-drying. The approach is particularly valuable when a formulation is sensitive to moisture, temperature, or long-term storage in liquid form. By removing water under controlled conditions, manufacturers can help protect the physical and chemical characteristics of suitable drug products while creating a dosage form that can be reconstituted before use. Kilitch Healthcare combines pharmaceutical development and manufacturing capabilities, making the overall process easier to view as an integrated product journey rather than as an isolated drying operation. Why Lyophilization Matters in Pharmaceutical Manufacturing Many pharmaceutical ingredients have stability challenges when maintained as aqueous solutions for extended periods. Moisture can contribute to degradation, changes in potency, or physical instability. Lyophilization addresses this challenge by freezing the formulation and then removing ice through sublimation under reduced pressure. The resulting dry product can offer improved stability for appropriately selected formulations, while also supporting defined storage and distribution requirements. However, freeze-drying is not automatically suitable for every medicine. The formulation, active ingredient, excipients, container system, intended route of administration, and target shelf life all influence whether lyophilization is appropriate. Effective development therefore starts with understanding the product before designing the manufacturing cycle. Key Stages of Lyophilized Drug Manufacturing 1. Formulation Development and Product Assessment The first stage is to evaluate how the formulation behaves during freezing and drying. Active pharmaceutical ingredients, excipients, concentration, pH, solubility, and thermal characteristics can all influence the process. Developers assess whether the formulation can produce an acceptable dried structure and whether the product will retain its intended performance after reconstitution. 2. Controlled Preparation and Sterile Filling For sterile products, formulation preparation and filling must take place under carefully controlled conditions. Depending on the product, manufacturing may involve compounding, filtration, transfer, and filling into suitable vials or other approved containers. Fill volume, component compatibility, and process controls need to be consistent before the units enter the lyophilization stage. 3. Freezing and Primary Drying Freezing determines the physical state in which the formulation enters the drying cycle. During primary drying, pressure and temperature are controlled so that frozen water is removed primarily through sublimation. The cycle must be designed around the characteristics of the specific formulation because an unsuitable combination of temperature, pressure, or duration can affect product structure and quality. 4. Secondary Drying and Final Moisture Control After primary drying, secondary drying removes additional bound moisture. The objective is to achieve a suitable residual moisture level without damaging the product. The final moisture profile can influence stability, so cycle development and testing are important in establishing repeatable manufacturing conditions. 5. Stoppering, Inspection, and Packaging Once the drying cycle is complete, containers are stoppered under controlled conditions. The container-closure system becomes part of the product protection strategy, helping preserve the dried formulation during storage and distribution. Finished units undergo appropriate inspection and quality testing before packaging and release. Critical Quality Considerations Formulation–Cycle Compatibility A robust lyophilization process depends on compatibility between the formulation and the cycle. Small changes in concentration, excipient selection, or composition can alter freezing behavior and drying performance. For this reason, formulation development and process development should progress together. Residual Moisture and Stability Residual moisture is an important quality attribute for many freeze-dried products. Too much remaining moisture may affect stability, while excessive drying can also be undesirable for certain formulations. Appropriate analytical testing and stability studies help establish product-specific targets and storage conditions. Container-Closure Integrity The vial, stopper, and seal must provide appropriate protection throughout the product’s intended shelf life. Compatibility with the formulation, integrity of the closure system, and protection against environmental exposure should therefore be considered during development rather than treated as final-stage packaging decisions. Aseptic Processing and Contamination Control When the finished product is sterile, contamination control is fundamental throughout manufacturing. Personnel practices, facility controls, equipment, material movement, environmental monitoring, and validated procedures work together to maintain the required level of sterility assurance. These controls must remain consistent from preparation through filling, lyophilization, stoppering, inspection, and release. Why an Integrated Manufacturing Approach Matters Lyophilized products require close coordination between product development, manufacturing, quality, and packaging teams. An experienced pharmaceutical manufacturing partner can help connect these functions so that development decisions are practical for commercial production. This is particularly important when a product moves from laboratory or pilot work into larger-scale manufacturing, where equipment differences and process controls can affect cycle performance. An integrated approach can also improve project coordination. Formulation requirements can be considered alongside filling capabilities, lyophilization equipment, container systems, analytical testing, documentation, and supply planning. This reduces the risk of discovering manufacturing constraints only after significant development work has been completed. Scale-Up Considerations for Lyophilized Products Moving a lyophilized product from development to commercial manufacturing requires more than increasing batch size. Heat and mass transfer characteristics can change with equipment configuration, load size, shelf arrangement, and process conditions. The manufacturing team must evaluate whether the established cycle remains appropriate and whether critical process parameters can be controlled consistently at the intended scale. Process knowledge is therefore essential during technology transfer and scale-up. Defined acceptance criteria, appropriate development data, equipment understanding, and documented procedures can help support a smoother transition. Commercial readiness should be assessed alongside product quality so that the final process is both scientifically sound and operationally repeatable. Choosing the Right Manufacturing Partner Companies evaluating lyophilized drug manufacturing should look beyond the availability of a freeze dryer. Important factors include formulation-development expertise, sterile filling capabilities, process-development experience, quality systems, analytical support, container-closure knowledge, documentation, and the ability to support commercial production. Lyophilized Drug Manufacturing at Kilitch Healthcare Kilitch Healthcare operates across pharmaceutical development and specialized manufacturing, with capabilities that include sterile injectable products in liquid and powder forms, along with ophthalmic and nasal formulations, prefilled syringes, and other healthcare products. Its manufacturing model brings research, development, production, and quality considerations into the same broader ecosystem. For companies exploring lyophilized pharmaceutical manufacturing, this
Drug Product Technology Transfer
Introduction: Why Technology Transfer Matters Drug product technology transfer is the structured process of moving product and manufacturing knowledge from a development environment, originating site or established process into a receiving manufacturing operation. The objective is to reproduce the product and process consistently while maintaining defined quality requirements. Kilitch Healthcare works across pharmaceutical development and specialized manufacturing, making technology transfer an important bridge between product development and commercial production. What Is Drug Product Technology Transfer? A drug product technology transfer brings together the technical information required for another team or manufacturing site to understand, reproduce and control an established pharmaceutical product. This can include formulation information, manufacturing procedures, process parameters, specifications, analytical methods, packaging requirements and relevant development knowledge. Technology transfer is not simply the exchange of documents. The receiving team needs to understand how the product behaves, which process variables are important and which controls are critical to maintaining quality. Effective transfer therefore combines documentation, technical communication, practical evaluation and appropriate verification. Key Stages of Drug Product Technology Transfer 1. Transfer Planning and Gap Assessment A successful transfer begins with a defined plan covering the sending and receiving teams, product scope, responsibilities, timelines and required information. A gap assessment can identify differences in equipment, facilities, materials, analytical capabilities and manufacturing procedures before transfer activities begin. This early assessment is valuable because a process developed using one set of equipment may not behave identically on another manufacturing platform. Identifying differences in advance allows the teams to determine which parameters require additional evaluation or adaptation. 2. Compilation of Product and Process Knowledge The transfer package should contain the information needed to understand the product and its manufacturing process. Depending on the dosage form, this may include formulation composition, material specifications, manufacturing instructions, critical process parameters, in-process controls, finished-product specifications, packaging information and stability data. Development reports and process knowledge can also provide useful context. They explain why particular conditions were selected and help the receiving team understand which variables may have the greatest impact on product quality. 3. Equipment and Process Evaluation The receiving site evaluates whether its equipment and manufacturing environment can support the transferred process. Differences in vessel capacity, mixing characteristics, filling equipment, temperature control or other operating features may affect process performance. The objective is to establish whether the existing process can be reproduced or whether controlled adjustments are required. 4. Analytical Method and Quality Transfer Analytical methods are an important part of technology transfer because they provide the measurements used to evaluate product quality. The receiving laboratory needs suitable procedures, specifications, reference materials and trained personnel. Method transfer or verification activities may be required according to the product and applicable quality requirements. 5. Trial Batches, Validation, and Commercial Readiness Where appropriate, engineering or demonstration batches can help evaluate the transferred process under receiving-site conditions. These activities generate practical information about equipment performance, material behavior and process controls. Further qualification or validation activities are then performed according to the established transfer and quality strategy. Technology Transfer and Pharmaceutical Scale-Up Technology transfer is closely connected with scale-up when a product moves from development or pilot manufacturing into larger commercial batches. Increasing batch size can change mixing, heat transfer, filling behavior and material movement. A process that performs well at development scale therefore needs to be assessed against the characteristics of commercial equipment. Scale-up should preserve the product’s established quality attributes while creating a process that can be operated consistently. Transfer teams use development knowledge and process data to understand which variables are most important and how they should be controlled at the receiving scale. Documentation and Knowledge Management Clear documentation provides the foundation for an effective technology transfer. Transfer protocols, reports, specifications, manufacturing instructions, analytical procedures and change records help establish traceability throughout the project. Documentation should also capture decisions made during the transfer so that the final commercial process reflects the knowledge gained during development and implementation. Technical communication is equally important. Meetings between formulation, process development, quality, analytical and manufacturing teams can help resolve questions that may not be obvious from written documents alone. This collaboration supports a common understanding of the product and its critical requirements. Common Challenges in Drug Product Technology Transfer Differences in Equipment and Facilities Equipment at the receiving site may differ in capacity, design or operating characteristics from the development setup. These differences can influence process behavior and may require additional assessment. A structured comparison of equipment and process requirements helps identify potential risks before manufacturing begins. Incomplete Process Knowledge A transfer can become more difficult when development information does not clearly explain process rationale or critical variables. Capturing development knowledge, including important process observations and historical decisions, can give the receiving team a stronger foundation for implementation. Communication Across Teams Technology transfer often involves multiple functions and organizations. Clear responsibilities, agreed documentation and regular technical communication can reduce misunderstandings and help keep transfer activities aligned with quality and commercial objectives. Why an Integrated Development and Manufacturing Partner Matters An integrated partner can connect formulation development, process development, manufacturing, analytical testing and quality activities throughout the transfer. This continuity can help reduce information gaps and make it easier to evaluate how development decisions translate into commercial production. pharmaceutical development and manufacturing capabilities are therefore relevant when companies are assessing a partner for a product that needs to move from development into routine supply. An integrated approach can also support faster identification of practical manufacturing constraints. When development and production teams work closely together, equipment suitability, process controls, packaging and testing requirements can be considered before commercial batches are scheduled. How to Evaluate a Technology Transfer Partner Companies evaluating a technology transfer partner should consider its experience with the relevant dosage form, development infrastructure, manufacturing capabilities, quality systems and analytical support. The partner should be able to understand technical documentation while also translating that information into controlled manufacturing activities. It is also useful to assess whether the manufacturer can support the full pathway from transfer through commercial supply. Businesses evaluating Kilitch Healthcare
Pharmaceutical Exporter From India: Strengthening Global Healthcare Through Quality Manufacturing
Discover how a pharmaceutical exporter from India supports global healthcare through quality manufacturing, regulatory compliance, and international pharmaceutical supply.
Pharmaceutical Contract Manufacturing: Driving Efficiency and Growth in the Pharmaceutical Industry
Explore how pharmaceutical contract manufacturing helps companies scale production, ensure quality compliance, and accelerate market growth worldwide.
Sterile Injectable Manufacturing: The Foundation of Safe Injectable Medicines
Discover the importance of sterile injectable manufacturing, aseptic pharmaceutical manufacturing, quality compliance, and global healthcare standards.
Eye Drops Manufacturer: Ensuring Quality in Modern Ophthalmic Production
Learn how an eye drops manufacturer ensures quality, sterility, and safety through advanced ophthalmic drug manufacturing and global compliance standards.
A Global Pharmaceutical Manufacturing Company Delivering Quality Worldwide
Discover how Kilitch Drugs supports global healthcare through ophthalmic drug manufacturing, sterile injectable manufacturing, pharmaceutical exports, and WHO-GMP compliant production facilities.
How Contract Drug Manufacturing Works
Introduction: Understanding Contract Drug Manufacturing Developing a medicine and bringing it to market requires more than a validated formulation. Businesses also need suitable facilities, equipment, trained teams, quality systems, testing capabilities and a controlled route to commercial production. Contract drug manufacturing provides a model in which a specialized manufacturing partner produces healthcare products on behalf of another company, allowing the product owner to access established infrastructure and technical expertise without building every manufacturing capability internally. The scope of a contract relationship can vary. Some projects focus mainly on commercial production, while others involve development support, scale-up, technology transfer, packaging and commercialization. Choosing the right partner therefore starts with understanding the product, its manufacturing requirements and the level of support needed. Companies evaluating contract drug manufacturing can use these factors to compare capabilities and establish a manufacturing pathway suited to their product and market objectives. What Is Contract Drug Manufacturing? Contract drug manufacturing is a business arrangement in which a manufacturer produces a drug or healthcare product for a client under agreed specifications and quality requirements. The client may own the formulation, brand or product rights, while the manufacturing partner provides the production infrastructure and operational expertise needed to make the product. The arrangement can be useful for companies that want to expand production without investing immediately in new facilities or specialized equipment. It can also support businesses entering new dosage forms or markets where specialized manufacturing knowledge is required. The exact responsibilities are normally defined through technical, quality and commercial agreements. Key Stages in Contract Drug Manufacturing 1. Product and Manufacturing Assessment Before production begins, the manufacturer and client need to understand the product’s formulation, dosage form, specifications, packaging requirements, expected volumes and applicable regulatory expectations. This assessment helps determine whether the available facility, equipment and quality systems are appropriate for the project. 2. Formulation Development and Process Optimization Some contract projects begin with a formulation that is already established, while others require development or optimization support. Development teams may assess ingredients, process parameters, stability considerations and manufacturing conditions. The objective is to create a process that can be transferred into controlled production while preserving the intended product characteristics. 3. Technology Transfer and Scale-Up Technology transfer is an important bridge between development and commercial manufacturing. Product knowledge, process instructions, analytical methods and critical parameters need to be communicated and documented. Scale-up then translates the process into larger production quantities while maintaining appropriate controls. A structured transfer can help identify equipment differences, process risks and documentation requirements before routine manufacturing begins. 4. Commercial Production Once the process is established, production takes place under defined procedures and quality controls. Raw materials, equipment, environmental conditions and process parameters are monitored according to the product and manufacturing requirements. Batch records and traceability systems support consistent execution and provide a documented history of production. Quality Control in Contract Manufacturing Quality Assurance Quality assurance provides the framework that keeps manufacturing activities controlled and documented. It can include standard operating procedures, training, validation, change control, deviation management, corrective and preventive actions, documentation review and batch release processes. These systems help ensure that manufacturing remains aligned with approved requirements. Quality Control Testing Quality control laboratories may evaluate raw materials, in-process samples and finished products against established specifications. Testing requirements depend on the dosage form and product characteristics. Consistent analytical procedures and accurate documentation are important because they support decisions about product quality and release. Regulatory and Documentation Requirements Contract manufacturing also involves significant documentation. Specifications, manufacturing instructions, test methods, batch records and quality agreements need to remain controlled and traceable. For companies supplying regulated markets, the manufacturer’s regulatory experience and documentation practices can be an important part of partner evaluation. Specialized Manufacturing Capabilities Not every contract manufacturer supports every dosage form. Sterile injectables, ophthalmic products, nasal formulations and prefilled syringes can require specialized facilities, equipment and environmental controls. A manufacturer’s technical capabilities should therefore be matched to the product rather than assessed only by overall production capacity. Kilitch Healthcare works across several specialized healthcare categories and describes capabilities involving sterile injectables, ophthalmic formulations, nasal formulations and prefilled syringes. Businesses researching Kilitch Drugs can consider these categories when assessing whether a potential manufacturing partner has experience relevant to their intended product. Technology can also differentiate manufacturing capabilities. Specialized processes such as preservative-free delivery, sterile applications and advanced filling or packaging technologies may be relevant for particular products. For clients considering Kilitch Drugs and related healthcare manufacturing requirements, understanding the technology behind production can be as important as understanding the facility itself. Benefits of Working With a Contract Manufacturer Access to Established Infrastructure Using an established manufacturer can give businesses access to production facilities, trained personnel, equipment and quality systems without requiring the same level of internal capital investment. This can be particularly relevant when a product requires specialized manufacturing infrastructure. Flexible Production and Scalability Contract manufacturing can also support changes in production volume. A product may move from initial commercial quantities to larger batches as demand develops. Manufacturers with appropriate capacity planning and scalable processes can help clients manage this transition while maintaining defined quality standards. Technical Collaboration A contract relationship can extend beyond manufacturing. Development, technology transfer, process optimization, quality and supply teams may need to collaborate throughout the product lifecycle. Clear communication and defined responsibilities can make this coordination more efficient. How to Choose a Contract Drug Manufacturing Partner Assess Product-Specific Expertise Start by checking whether the manufacturer has relevant experience with the dosage form, manufacturing environment and product category. A partner’s expertise should correspond to the actual technical requirements of the project. Review Quality Systems Evaluate quality assurance, testing, validation, documentation and regulatory practices. Companies should understand how deviations, changes, batch records and product release are managed before entering a long-term manufacturing relationship. Consider Long-Term Supply Requirements Manufacturing should be considered as part of the product lifecycle rather than a single production event. Capacity, lead times, packaging, technology transfer and future scale-up should all be discussed early so that the relationship can support changing commercial